From crude preheat trains to vacuum condensers and fin-fan coolers, refinery service demands fin tubes that hold their performance through thermal cycling, vibration and corrosive streams.
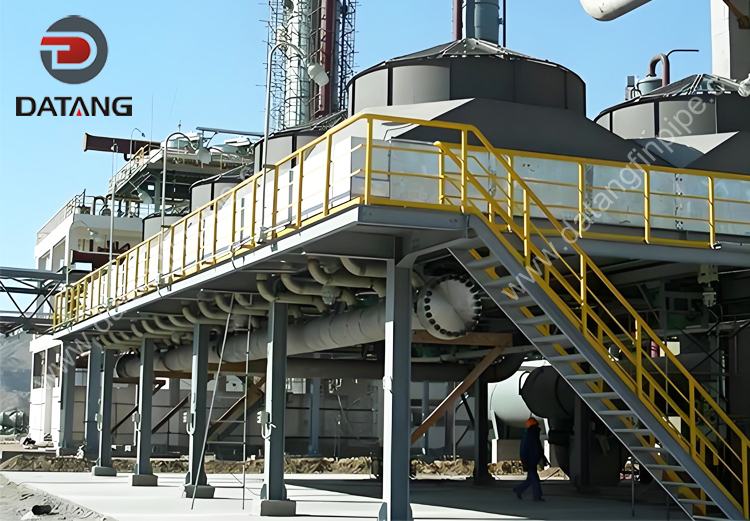
Where finned tubes are used in a refinery
- Air-cooled condensers and coolers on crude, vacuum, naphtha, kerosene and diesel streams.
- Fired heater convection sections and air preheaters.
- Fin-fan coolers on lean/rich amine, glycol and cooling-water circuits.
- Overhead condensers where the tube material must resist wet H₂S and chlorides.
Material selection
Carbon steel A179 and A192 cover most hydrocarbon duties. For wet sour service we recommend stainless or alloy base tubes with the same fin geometry, and for high metal temperatures the embedded (G) fin or HF welded construction. Our engineers will confirm the base tube standard and the required wall thickness once the design pressure and corrosion allowance are known.
Fouling and cleaning
Air-side fouling in refineries is usually handled by soot blowing and water washing. Wide fin pitches (3.2–4.5 mm) and thicker fins make cleaning easier and reduce the risk of fin damage during maintenance. Where the air stream carries dust or catalyst fines, studded tubes remain the safest choice.
| Service | Recommended tube | Reason |
|---|---|---|
| Crude overhead condenser | Embedded G, stainless base | Wet H₂S and chloride resistance |
| Vacuum tower condenser | Extruded bimetal, large diameter | Low pressure drop, high surface |
| Amine cooler | Extruded or L/LL | Clean stream, cost efficiency |
| Flue gas / air preheater | HF welded or double-H | High temperature, ash |
Send your refinery tube list
Tell us the tube diameter, fin height, fin pitch, materials and quantity — we reply with price and lead time within one working day.