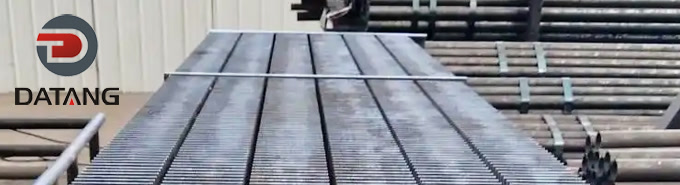
A steel strip is fed onto the rotating base tube while a high-frequency current melts the interface. The strip is wound into a helix and welded continuously along its foot, so fin and tube are fused into one metallurgical joint.
That bond survives conditions that destroy wrapped fins: flue gas, soot-blower erosion and metal temperatures up to 600 °C, higher with matching alloys. HF welded tubes are the standard choice for boiler economisers, air preheaters, HRSG modules and waste-heat recovery.
Base tubes and fins are available in carbon steel, stainless steel and alloy steel grades including T11, T22, P5 and P9. For coal-fired and biomass duties we recommend a minimum fin thickness of 1.0–1.5 mm and a pitch wide enough to avoid ash bridging; serrated fins can improve heat transfer in clean gas streams.
Send the flue gas composition, dust load, design temperature and pressure, and we will propose the tube and fin geometry.
Related: High Frequency Welded Finned Tube · Laser Welded Fin Production · L / LL / KL Fin Winding